PETG 3D Printing: Properties, Settings and Best Practices
PETG 3D Printing: Properties, Settings and Best Practices
Quick verdict: PETG is the filament to reach for when a part must be tougher than PLA but does not need the heat resistance of ABS. It bonds its layers willingly, shrugs off humidity and most workshop chemicals, and prints on an open machine with a heated bed and an all-metal hotend. Its reputation for stringing, and for gripping the build plate harder than you expect, is earned. Both problems have straightforward fixes, and once those are handled PETG becomes the most predictable functional filament in a workshop.
PETG sits between the two filaments most workshops already keep on the shelf. It prints hot, like ABS, yet it fuses its layers far more readily and barely warps. Against PLA it is softer, springier, and much harder to break.
What follows is a working guide: what the material is, the published properties that decide whether it suits your part, the printer and slicer settings to start from, the stringing and bed-adhesion faults PETG is known for, drying and storage, the safety caveats that matter before a printed part goes near food or heat, and where PETG earns its place in a Malaysian workshop.
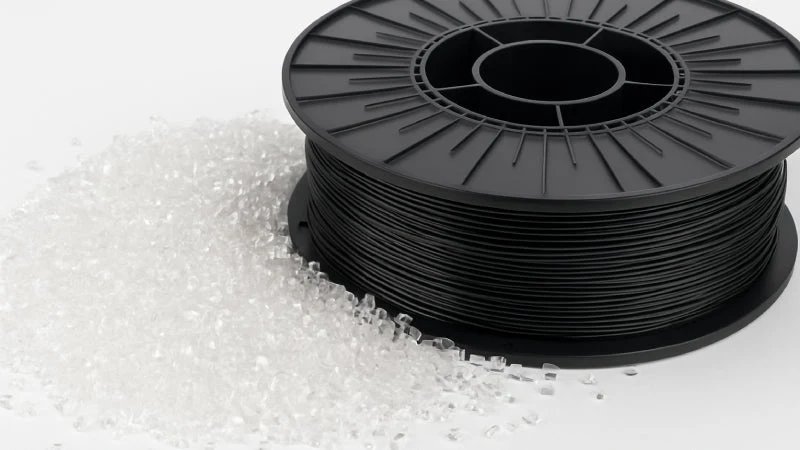
PETG arrives as translucent pellets and leaves the extruder as filament; the same material behaves differently in each form
What PETG is, and how it differs from PLA and ABS
PETG is a copolyester. The name stands for polyethylene terephthalate glycol-modified, which describes both the base polymer and the change made to it. Plain PET is the clear plastic of drink bottles: strong, stiff, and awkward to print because it crystallises as it cools. Introducing glycol during polymerisation disrupts that crystallisation. What comes out is an amorphous plastic that stays clear, flows at a workable temperature, and sets without pulling against itself.
Three consequences follow from that chemistry, and between them they explain almost everything about printing PETG.
Low shrinkage. There is no crystal structure snapping into place during cooling, so contraction is small. A large flat PETG part usually stays flat without an enclosure.
Ductility rather than brittleness. Where PLA snaps under the first serious load, PETG bends, whitens along the fold, and keeps holding.
Moisture uptake. The same chemistry that makes the material resist water also lets it draw moisture out of humid air over weeks. Drying matters more here than it does for PLA.
Set against ABS, the argument is about heat and solvents. ABS carries load close to 100°C; PETG softens nearer 80°C and creeps above roughly 70°C under sustained stress. ABS also stands up to fuels, oils and concentrated alkalis better, and it can be vapour smoothed to a glossy skin. What ABS cannot do is print without an enclosure or a heated chamber, and it releases styrene while it prints. PETG needs neither the enclosure nor the same level of extraction. That difference alone has moved a lot of workshop production from ABS to PETG.
Against PLA, PETG is a durability upgrade paid for with a little precision. PLA is stiffer and holds fine detail on small features. PETG is tougher, handles humidity and sunlight better, and does not sag in a parked vehicle on a hot afternoon.
PETG material properties
The values below are the ones commonly published for PETG filament. Read them as typical numbers for a standard formulation rather than guarantees; the datasheet that ships with your spool always takes precedence.
Property
Typical PETG value
What it means for your part
Tensile strength
Around 50 MPa
Enough for brackets, housings and machine guards
Elongation at break
Around 120%
Bends a long way before failure, which is the sharpest difference from PLA
Flexural modulus
Roughly 2,100 MPa
Stiffer than any flexible filament, softer under load than PLA
Impact behaviour
Well ahead of PLA in the notched impact test, behind ABS
Absorbs knocks without shattering, but not a material for repeated heavy strikes
Hardness
Shore D 76-80
Resists scratching in handling, softer than PLA at the same test
Glass transition temperature
Around 80°C
Holds shape in a warm workshop; continuous service is realistic up to roughly 70°C
Density
1.27 g/cm³
Denser than PLA or ABS, so a printed part has a more solid feel for the same volume
Chemical resistance
Good against acids, alcohols, oils, fuels and most detergents; poor against strong alkalis and some solvents
Suits fluid handling and wash-down areas, but check the specific chemical first
UV and weather resistance
Moderate, clearly better than PLA, well behind ASA
Fine for shaded outdoor use and humid interiors; long-term direct sun is ASA territory
Water resistance
Low uptake, does not degrade in splash or humidity
Suitable for parts that see condensation, wash-down or monsoon air
Shrinkage
Low, well below ABS
Large flat geometry prints flat without a chamber
Four rows carry most of the decision. Elongation at break is why a PETG part survives a drop that would crack PLA. The glass transition temperature is why a PETG bracket lives happily on a workshop wall but sags if it is bolted to a hot machine surface. Chemical resistance is what lets PETG sit in contact with oils, coolant and cleaning fluids. And low shrinkage is why it prints reliably on an open machine, which is exactly where ABS fights you.
PETG also machines and finishes cooperatively. It drills and taps without cracking if the tool is sharp and the feed is light, it can be sanded smooth, and small areas can be shaped with gentle heat. Clear PETG can be polished back to a degree of transparency after printing, which is useful for light covers and inspection windows. Sanding takes patience because the material is soft and loads abrasive paper quickly.
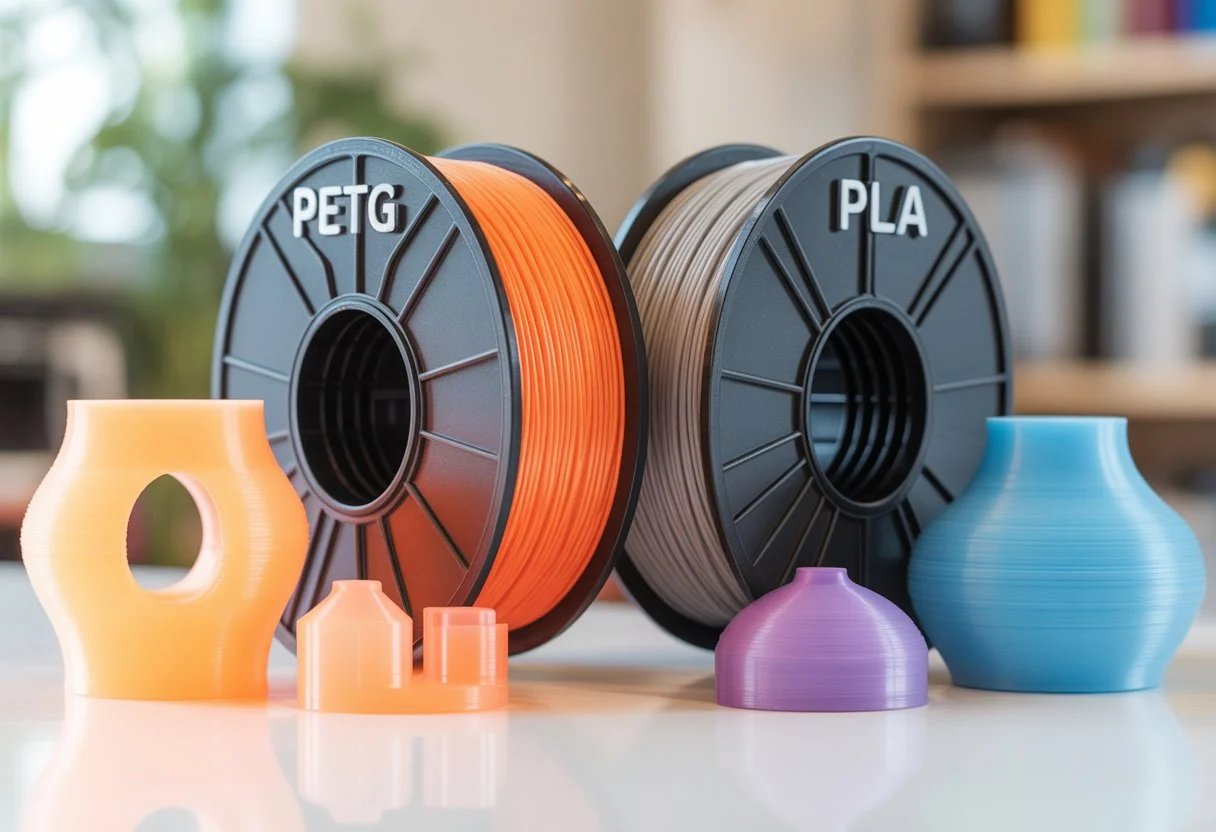
The two filaments look alike on the spool but differ in toughness, temperature resistance and how willingly they bond
How PETG compares with PLA, ABS and ASA
Choosing PETG is really a question of what your part has to survive. The table below places it against the other filaments you are likely to be offered.
Material
Heat resistance
Toughness
Print demands
Where it wins
PETG
Softens near 80°C, creeps above about 70°C
High, with strong layer bonding
Nozzle 230-250°C, bed 70-80°C, all-metal hotend preferred, no enclosure needed
Jigs, guards, brackets, chemical and humidity exposure, general functional parts
PLA
Low; a hot vehicle interior is enough to deform it
Stiff and brittle
Easiest of the group, no heated bed strictly required, no odour
Concept models, display pieces, quick shop fixtures with no load
ABS
Continuous use near 100°C
Highest of the three under repeated impact
Nozzle to 250°C, bed at 95-110°C, enclosure and ventilation
Automotive interior hardware, parts near engine heat, vapour-smoothed housings
ASA
Similar to ABS
Similar to ABS
As ABS: enclosure and a hot bed
Outdoor and sun-exposed parts where ABS would chalk and fade
Nylon
Higher than ABS
Highest of the group, with strong abrasion resistance
Higher temperatures, dry filament, disciplined moisture control
Gears, wear surfaces, living hinges, sustained chemical contact
PLA versus PETG is the commonest comparison, and the answer depends on whether the part does anything. A PLA display model is a better model. A PLA bracket that gets clamped, dropped or left in a car is a part you will reprint. PETG costs a little more print time and a little more tuning, and it pays that back the first time a part survives an accident.
PETG versus ABS comes down to temperature. If the part is going somewhere above 70°C, in a vehicle, near a heater, beside an extruder or on a machine that runs all day, PETG will creep and lose its fit. That is a hard limit, not a tuning problem. Everywhere below that line, PETG is the easier material to live with: no chamber, less odour, better layer bonding, and far less warping on large geometry.
ASA exists for one reason ABS and PETG both fall short: long exposure to sunlight. Where a part lives outdoors on a machine guard, a sign frame or vehicle exterior, ASA holds its colour and surface far longer. PETG handles the humidity and rain of a Malaysian climate well enough, but years of direct ultraviolet light will dull it, so a sunlit outdoor part should be ASA or a coated PETG part rather than bare PETG.
When to choose PETG over PLA, ABS or ASA
The decision is usually obvious once the service conditions are written down.
Choose PETG for jigs, fixtures and assembly aids that get handled every shift.
Choose PETG for parts exposed to water, condensation or high humidity, where PLA loses stiffness over time.
Choose PETG for contact with oils, coolants, acids and most cleaning chemicals.
Choose PETG when the part needs to flex slightly and return, such as clips, snap fits and protective covers.
Choose PETG when you want functional parts from an open printer with no enclosure and no chamber.
Choose ABS or ASA when service temperature climbs above roughly 70°C, or when a part faces years of direct sun.
Choose nylon for gear teeth, sliding wear surfaces and sustained exposure to aggressive chemicals.
Choose PLA when the part is a model, a visual aid or a fixture that carries no load and stays cool.
Printer requirements for PETG
PETG is undemanding by engineering-plastic standards, but it does have a short list of requirements.
A hotend that reaches 250°C. Most working PETG profiles sit between 230°C and 250°C. A hotend with a PTFE liner inside the melt zone starts to degrade above roughly 240°C, so an all-metal hotend is the safer choice if PETG will be a regular material. This is standard on the FDM machines from CreatBot and most current desktop printers from Bambu Lab and FlashForge.
A heated bed that holds 70-80°C. A cold bed will not keep a PETG first layer down. Any heated bed reaches the low end of that range; a bed that reaches 80°C comfortably gives you more room on large flat parts.
No enclosure. This is where PETG beats ABS in practice. It prints happily on an open machine. If your printer is enclosed, leave a door or lid open during long jobs so chamber heat does not creep toward the glass transition temperature and soften the part on the plate.
A standard nozzle. PETG is not abrasive, so a brass nozzle is fine. That changes the moment you move to a carbon fibre or glass fibre blend, which needs a hardened nozzle and slightly wider settings. The same printer handles both, but the tooling does not.
Direct drive if you have the choice. Stringing control is easier when the extruder sits close to the nozzle, because retraction only has to relieve pressure over a short distance instead of pulling filament back through a long tube.
A part cooling fan that works. Unlike ABS, PETG wants a measured amount of cooling. Print the first layer with the fan off, then bring it up modestly.
Machines built around high-temperature materials, including the heated-chamber industrial lines from Intamsys, will run PETG without effort, but nothing in that class is required for it. A well-set open printer is enough.
PETG slicer settings
Treat this table as a starting point for a standard PETG formulation, then adjust in small steps toward your own part.
Setting
Starting point
Why
Nozzle temperature
230-250°C, with 240°C a sensible first try
Too cool and layers will not fuse; too hot and the stringing gets worse
Bed temperature
70-80°C
Holds the first layer flat without the aggressive heat ABS needs
Print speed
40-60 mm/s
Pushing past this weakens layer bonds and exaggerates oozing
First layer speed
Roughly half your normal print speed
A slow first layer lets the material settle instead of being dragged
Layer height
0.1-0.3 mm
Thicker layers bond better and hide small surface flaws, thinner ones look sharper
Part cooling fan
Off for the first layer, then 20-50%
Enough cooling to set overhangs, not enough to starve layer bonding
Retraction
1-3 mm direct drive, 4-6 mm through a Bowden tube, at 20-40 mm/s
The single most important setting for stringing; Bowden setups need the longer pull
Travel moves
Enable z-hop and travel avoidance so the nozzle crosses printed material rather than open air
Cuts the web of strings left behind empty travel
Wall thickness
Minimum 1.2 mm on functional parts, ideally three perimeters
Thin walls make a part that cracks at the first knock
Infill
20-40%, rising to 50-60% for load-bearing parts
Match density to the load instead of defaulting to solid
Two habits make those numbers work harder. Dry the spool before a long or visible print, because moisture turns good settings into a rough, bubbly surface. And change one variable at a time when you tune: temperature first, then retraction, then cooling.
Build surface and first-layer adhesion
PETG has an unusual failure mode. It rarely refuses to stick. It sticks too well. On bare glass and on smooth PEI, a PETG part can bond strongly enough to pull fragments out of the plate when you remove it, which is an expensive accident in a shop with a large-format machine. The fix is a release layer.
Glue stick on glass. The glue acts as a release agent, not as an adhesive. Applied thinly, it lets a PETG part grip while hot and lift cleanly once the bed cools.
Textured PEI. The texture gives the part a mechanical grip without the chemical welding you get on smooth surfaces, and it releases reliably at room temperature.
First layer temperature. Run the bed at the top of the working range for the first layer so the material spreads properly, then let it fall back if your profile allows.
Brim for large flat parts. A brim adds holding area at the corners without the material cost of a raft.
Clean the plate. Fingerprint oils are the usual cause of a first layer that grips in the middle and lifts at the corner.
Let the plate cool before removing the part. A warm PETG part is far more likely to deform as you pry it off than a cold one.
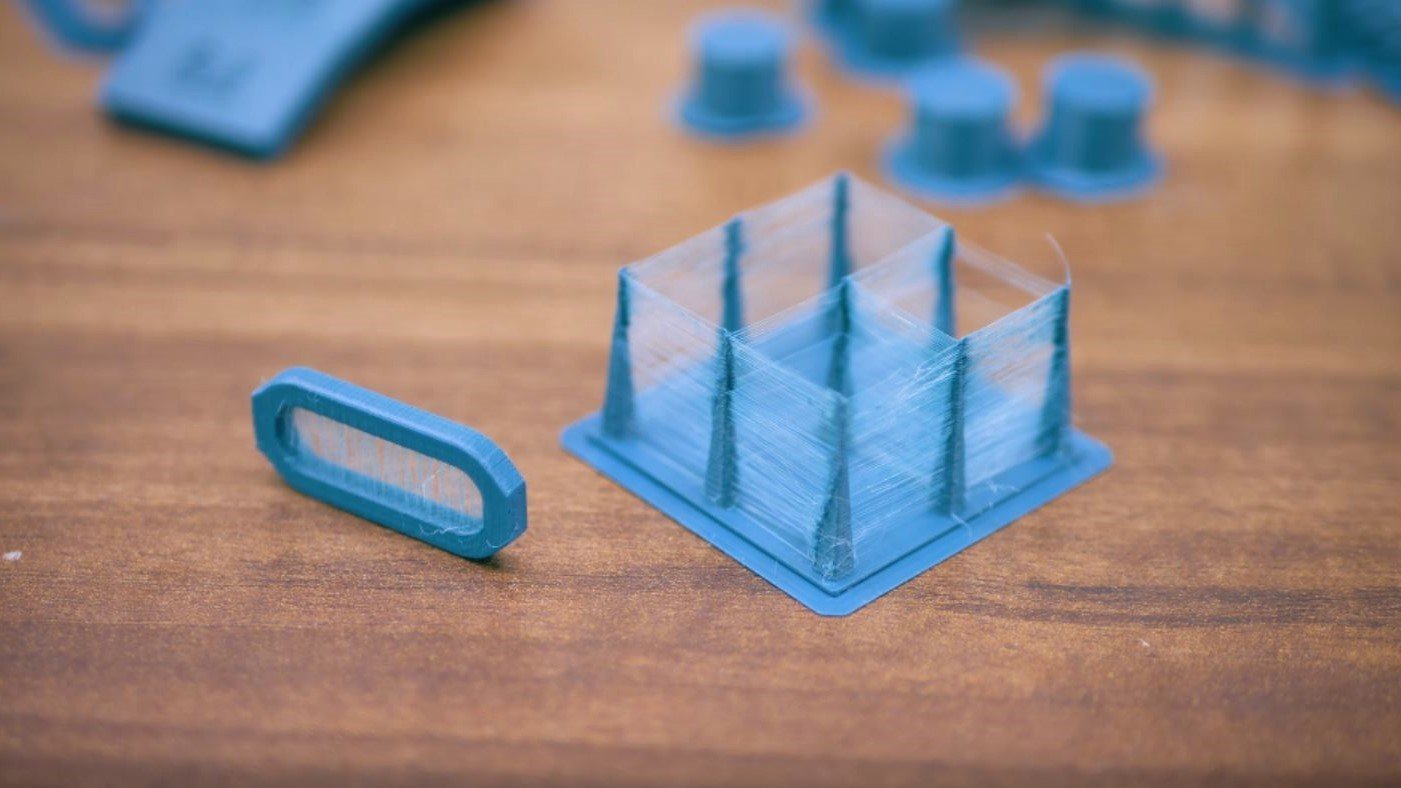
Stringing is the signature PETG fault: the nozzle keeps extruding as it travels and leaves a web between the walls
Solving stringing in PETG prints
Fine webs between separate features are the defining PETG annoyance. The cause is always the same: molten plastic keeps flowing out of the nozzle while the head travels through open air. Work through these in order, because the first two steps solve most cases.
Dry the filament. Moisture flashes to steam in the melt zone and pushes material out of the nozzle. Wispy strings that snap cleanly, plus a crackling or popping sound during extrusion, point straight at wet filament.
Lower the nozzle temperature in 5°C steps. Take it down until stringing drops away, then stop before layer bonding starts to suffer. Pulling a test part apart by hand tells you where that line sits.
Increase retraction distance and speed. A Bowden printer needs noticeably more distance than a direct-drive one because the pressure has to be relieved through the tube.
Turn on travel avoidance and z-hop, so the nozzle crosses over already printed material wherever the slicer can route it that way.
Raise the travel speed. Less time in free air means less time to ooze.
Trim the flow slightly if the surface looks over-packed. Less pressure in the nozzle means less material to leak out.
Clean the nozzle before starting. A dirty nozzle drags a thread through everything it touches.
Finish by hand. A quick pass with a deburring tool or a brief flash from a heat gun removes the last wisps. Keep the heat moving, because PETG softens at a low temperature and a part left under a hot gun will droop.
Warping, elephant foot and other PETG faults
PETG is far better behaved than ABS, but it has its own set of habits. The table below maps the symptom to the cause and the correction.
Symptom
Likely cause
Fix
Webbing and hairs between parts
Wet filament, nozzle too hot, retraction too short
Dry the spool, drop the temperature, raise retraction, enable travel avoidance
Part welded to the build plate
PETG bonding chemically to smooth glass or smooth PEI
Glue stick as a release layer, switch to textured PEI, cool fully before removal
Corners lifting on a large flat part
Draughts, low bed temperature, cooling on the first layer
Shield the printer from airflow, run the bed at 80°C, fan off for layer one, add a brim
Bulging elephant foot at the base
First layer squashed too hard into the plate
Reduce the first-layer squish, raise the nozzle a fraction, chamfer the bottom edge in the model
Layers splitting under load
Nozzle too cool, cooling too strong, printing too fast
Move into the 240-250°C band, cut the fan back, slow down, increase wall count
Rough, milky or bubbling walls
Moisture boiling in the melt zone
Dry the filament before printing and store it sealed afterwards
Blobs and zits on the surface
Over-extrusion or accumulated ooze
Trim the extrusion multiplier, check filament dryness, wipe the nozzle mid-print
Warping deserves one clarification. PETG will not warp the way ABS does on a large panel, which is why an enclosure is not needed. It can still lift at corners when a draught crosses the plate or the bed runs cool, and the answer is usually airflow rather than heat. Position the printer away from an air-conditioning vent or an open doorway, and most of this problem disappears.
Drying and storing PETG
PETG absorbs moisture more slowly than nylon and faster than PLA, which is why a spool left open in a Malaysian workshop will print well for a while and then start misbehaving with no change to the settings. Common signs are popping during extrusion, a dull or bubbly surface, weaker layer bonding and more stringing than the same spool produced a month earlier.
The remedy is straightforward. Dry the spool at around 65°C for four to six hours, longer for a spool that has been open for weeks, using a purpose-built filament dryer rather than a domestic oven that cannot hold a low, steady temperature. A vacuum or resealable bag with fresh desiccant keeps the filament dry between jobs, and a sealed storage box with a hygrometer makes the state of every spool visible at a glance.
Two practical points. Dry the spool before any print where surface finish or strength matters, not only when a problem has already appeared. And never assume a factory seal means dry filament, because vacuum packaging does not guarantee the filament was dry when it was packed.
Food contact, fumes and safety caveats
The chemistry of PETG is well understood and the base polymer is used in food packaging, which is why PETG has a reputation as the food-safe printing material. That reputation needs qualification, because the risk comes from the printing process rather than the plastic.
Layer lines harbour bacteria. A printed surface is not smooth. The crevices between layers and the open cells inside infill give microbes a place to sit that is difficult to clean. This applies to any FDM material, not only PETG.
Nozzles are not all inert. Brass nozzle alloys can contain small amounts of lead as an alloying element, and that is a documented concern for any surface that touches food. A plated or stainless nozzle removes that variable.
Nothing printed on a desktop machine is certified for food contact. If your product needs that claim, it needs the certification chain, not just the right polymer.
Hot food and dishwashers are out of range. PETG softens near 80°C, so it is unsuitable for hot drinks, hot-fill containers and dishwasher cycles.
Fumes are mild but not zero. PETG does not release styrene the way ABS does, and most operators find the odour far less noticeable. Fused deposition still emits ultrafine particles, so ventilate the print area and do not run long unattended jobs in a room where people sleep.
No fire rating. PETG is not a flame-retardant material. Do not substitute it for a rated plastic in electrical or fire-safety enclosures that require one.
Where PETG earns its place in Malaysian workshops
The mix of toughness, humidity tolerance and chemical resistance maps well onto shop-floor work, especially in a climate that is humid most of the year.
Jigs, fixtures and assembly aids. Handled every shift, dropped occasionally, and cheap to reprint when a design changes.
Machine guards and covers. Duct covers, terminal shields and access panels that need to flex into place without cracking.
Brackets, clips and cable management. The classic PETG job: a part that carries a modest load and has to survive being installed by hand.
Fluid and chemical handling. Drip trays, funnels, pipe clips and pump fittings for oils, coolants and mildly acidic or alkaline solutions. Verify the specific chemical, and do not use PETG for hot fluids or concentrated alkalis.
Humid or wet environments. Wash-down areas and covered outdoor installations where PLA would soften and lose stiffness.
Control and instrument housings. PETG insulates electrically and machines cleanly for cut-outs, where a flame rating is not required.
Retail and display parts. Point-of-sale fixtures, sign holders and product mock-ups, with clear PETG for light-diffusing covers.
Prototypes that must be tested. A PETG prototype survives assembly, fit checks and handling that would crack the same design in PLA.
Equally worth knowing is where PETG does not belong. Anything bolted to a hot machine surface, sitting in full sun for years, taking repeated heavy impacts, or needing a documented fire rating should go to another material. PETG is a general-purpose engineering filament with a clear ceiling, and the ceiling is about 70°C.
Frequently asked questions
Is PETG stronger than PLA?
In different ways. PLA is the stiffer material, so a thin PLA part resists bending better until it snaps. PETG is far more ductile: it stretches around 120% before breaking, takes impacts without shattering, and resists humidity. For parts that carry a load but must not crack, PETG is the stronger choice in practice. For parts that need to hold a precise shape with no load, PLA will feel more rigid.
Why does my PETG string so badly?
Three causes, in order of likelihood. Wet filament is first, because moisture turns to steam and pushes molten plastic out of the nozzle. The nozzle temperature is second, since PETG oozes more the hotter it runs. Retraction is third, and it is the setting most often left on a PLA profile. Dry the spool, drop the temperature 5°C at a time, then work on retraction and travel moves.
Does PETG need an enclosure or a heated bed?
No enclosure, yes heated bed. PETG prints on open machines and does not need the warm chamber ABS requires. It does need a bed at 70-80°C to hold the first layer. If your printer is enclosed, leave it open so the chamber does not heat up and soften the part on the plate.
Can PETG be used outdoors in Malaysia?
For humidity, rain and shaded outdoor use, yes. PETG absorbs very little water and does not degrade in a tropical climate. Ultraviolet light is the limiting factor: direct sun dulls the surface and colour over time, so a part that faces the sky for years is better in ASA, or in PETG behind a coat of paint.
Is PETG food safe?
The polymer itself is used in food packaging, but a printed part is not a food-grade product. Layer lines and infill leave crevices that are hard to clean, brass nozzles can carry trace lead, and a desktop print carries no certification. For an implement that never touches food, PETG is a sensible choice. For a surface that does, treat it as unfit for that duty.